Ammonia Synthesis Catalyst Pressure Drop Fines and Bed Loading

Rising converter pressure drop is not always a catalyst activity problem. In many plants, the restriction is mechanical: broken particles, accumulated fines, the wrong granule range or an uneven catalyst bed.
The symptoms can look similar. Loop circulation becomes harder, compressor load rises, gas distribution deteriorates and production has less operating margin. Replacing the charge with “the same number of tonnes” will not solve the problem if the particle size, loading density or bed condition is wrong.
For an catalizador de síntesis de amoníaco replacement, the first job is to identify where the pressure loss starts and why it is increasing.
Tabla de contenido
Confirm Where the Pressure Drop Comes From
Compare differential pressure at similar gas flow, pressure, temperature and gas composition. Raw readings from different plant rates are not directly comparable.
Check whether the rise is across the whole converter or concentrated in one bed. Also verify the impulse lines and pressure transmitters. A restricted tapping point can look like a blocked catalyst charge.
| Pressure-drop pattern | More likely cause | What to review |
|---|---|---|
| High immediately after start-up | Wrong particle range, loading fines, excessive compaction or debris left in the bed | Catalyst certificate, screening record, bed height and loading report |
| Gradual rise during the campaign | Attrition, particle fracture, dust carryover or bed movement | Normalised ΔP trend, upstream condition and shutdown samples |
| Sudden increase after a trip | Bed shift, thermal event, internals problem or instrument fault | Trip history, temperature excursion and transmitter check |
| Different behaviour between beds | Local fines build-up, uneven packing or gas maldistribution | Bed-by-bed ΔP, temperature profile and converter internals |
| Pressure drop rises with falling conversion | Restricted flow or channeling may be affecting catalyst use | Gas distribution, bed profile and converter performance |
A stable pressure drop that only rises when throughput rises may reflect normal hydraulic behaviour. A normalised trend that continues climbing needs investigation.
Fines Close the Open Space Between Particles
Gas moves through the voids between catalyst particles. When small fragments and dust collect in those voids, the effective flow area becomes smaller. The gas then needs more pressure to pass through the bed.
Fines can come from transport damage, excessive drop height, rough transfer equipment or disturbance of the loaded surface. They may also develop through crushing, bed movement, operating upsets or upstream dust carryover.
Johnson Matthey’s review of catalyst structural breakdown(matthey.com/documents/161599/175071/Hetcat%2BDeactivation%2BWhitepaper%2BFinal.pdf/1c19fb4a-945a-8000-f711-939f9210fed5?t=1688132569754) distinguishes attrition, which erodes particles into fines, from fracture during loading or crushing in a fixed bed. That distinction matters. If fresh material reaches the converter with too many fragments, the starting ΔP may already be high. If fines develop in service, the pressure loss normally grows with time.
Do not assume that screening alone fixes every case. Screening can remove loose undersize material before loading, but it cannot repair weak handling, an incorrect loading method or continued dust carryover. Screening limits and procedures should come from the catalyst supplier or converter licensor.
Particle Size Is a Converter Decision
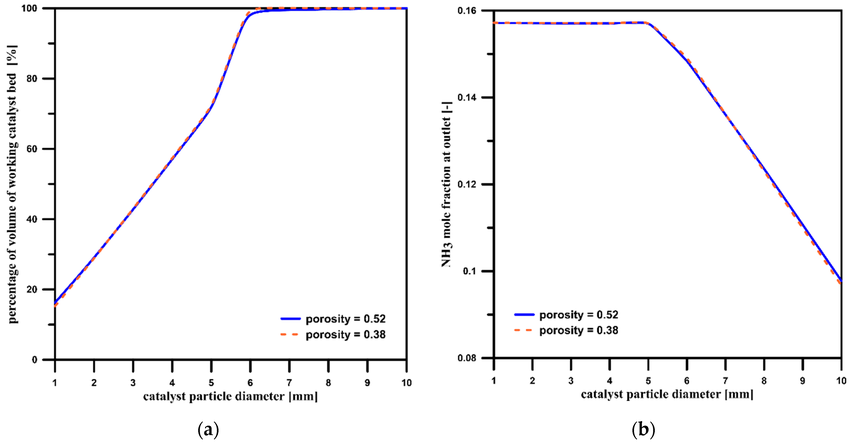
Smaller granules provide more external surface and shorter diffusion paths, but they also create narrower gas passages. Larger particles normally reduce bed resistance, although moving to a larger size can change catalyst volume activity and temperature behaviour.
This is why ammonia synthesis catalyst size should not be chosen by a simple “smaller is more active” rule.
The correct range depends on converter design, gas velocity, allowable bed ΔP, bed depth, support screens, gas distribution and the required heat-release profile.
Computational work on an axial-radial ammonia converter(mdpi.com/1996-1073/16/18/6680) confirms the basic trade-off between particle diameter, pressure loss and reactor performance. The purchasing lesson is more practical: do not change particle size without checking the converter duty.
For a replacement project, the current proven size is the starting reference. A different granule range may be suitable, but it should be reviewed against the licensor requirement, bed arrangement and available pressure-drop margin. Mixing sizes or creating graded layers without an approved loading plan can cause segregation and unpredictable flow.
Uneven Loading Creates Dense Zones and Bypass Paths
The right particle size can still perform poorly when the bed is loaded unevenly.
High-density pockets create extra resistance. Low-density areas or voids let gas bypass part of the charge. The converter may then show an uneven temperature profile even when the ammonia synthesis iron catalyst itself is active.
This risk is especially important in radial-flow beds. Gas takes the easiest route, so local variations in packing density can affect how much of the catalyst inventory is actually being used.
Johnson Matthey’s ammonia catalyst handling guidance recommends uniform bulk density to maintain consistent pressure-drop characteristics. It also warns that voids in radial beds can allow gas to bypass sections of the charge.
A controlled loading job should record the mass placed in each bed, usable volume, final height, package numbers, visible dust, screening results, transfer method and final surface condition.
These records become the baseline if pressure drop is high after start-up.
Particle Breakage Can Begin Before the Catalyst Arrives
Mechanical quality matters, but logistics and site handling also affect the final bed.
Check packaging when the shipment arrives. Look for damaged drums, loose closures, moisture exposure and abnormal dust. Store and move the material according to the supplier’s instructions.
Pre-reduced catalyst requires its specified handling and safety procedure. Damage to its protective oxide layer can expose reduced material to air and create self-heating risk. The loading method must therefore cover both mechanical protection and safe atmosphere control.
If the plant has experienced high ΔP before, request particle-size distribution and physical-quality documentation. A specification match is more useful than a generic statement that the product is an iron catalyst for ammonia synthesis.
Use Bed Volume, Bulk Density and Loaded Mass Together
The old purchase-order weight is not enough to size a new charge.
Required mass depends on the available bed volume and the loaded bulk density of the selected grade. Oxidised and pre-reduced catalysts can have different bulk densities. Particle range and loading practice can also affect how the material packs.
Before issuing a purchase order, reconcile three numbers:
Available bed volume × expected loaded bulk density = estimated catalyst mass
Compare the estimate with the historical loading record and final bed height. Resolve any major mismatch before shipment. Do not force excess material into the converter. Over-compaction increases resistance, while underfilling changes the intended bed geometry.
What HONREL Needs for a Replacement Review
Suministros HONREL iron-cobalt ammonia synthesis catalyst in oxidised and pre-reduced forms. Available particle ranges include 1.5–3.0, 2.2–3.3, 3.3–4.7, 4.7–6.7, 6.7–9.4 and 9.4–13.0 mm.
That does not mean every size fits every converter. HONREL should first match the proposed ammonia synthesis converter catalyst to the existing duty.
| Information to send | Por qué es importante |
|---|---|
| Current catalyst grade and TDS or COA | Establishes the existing specification |
| Current particle-size range | Sets the hydraulic and loading reference |
| Converter type and number of beds | Identifies axial, radial or combined flow requirements |
| Bed dimensions or usable volume | Supports quantity calculation |
| Previous loaded mass and final bed height | Checks historical packing and bulk density |
| Oxidised or pre-reduced condition | Affects loading weight, handling and start-up |
| Start-of-run and current pressure drop | Shows whether the restriction was present from loading or developed later |
| Gas rate, pressure and temperature with each ΔP reading | Allows a meaningful operating comparison |
| Photos or analysis of fines, if available | Helps separate transport damage, loading breakage and in-service attrition |
| Required delivery date and destination | Supports a workable replacement schedule |
With these details, HONREL can review particle size, grade, estimated charge and supply condition before quotation. This reduces the risk of repeating the previous loading problem.
For product matching, send HONREL the current size, bed volume and previous charge weight. Contact HONREL for an ammonia synthesis catalyst specification review and bulk supply quotation.