Zinc Oxide Catalyst for Natural Gas Desulfurization and H2S Removal

A zinc oxide catalyst is usually the last sulfur barrier before natural gas reaches a reformer, hydrogen unit, ammonia plant or another sulfur-sensitive process. Its job is simple: keep H2S slip below the downstream limit and protect the expensive catalyst that follows.
That does not make every ZnO grade interchangeable. Temperature, inlet sulfur, organic sulfur species, gas hourly space velocity and bed loading all affect performance. A product chosen by ZnO percentage alone may look acceptable on paper and still break through early.
HONREL 공급품 산화아연 탈황제 grades for low-, normal- and elevated-temperature gas purification. Send us your feed analysis and operating window, and we can compare the duty with a suitable grade and loading quantity.
목차
Where Does Zinc Oxide Fit in Natural Gas Desulfurization?
ZnO is normally used for polishing, not for carrying the full load of a raw gas stream with a high H2S concentration.
Bulk acid gas removal may come first. Depending on the plant, this could be an amine unit or another primary treatment step. If the feed contains mercaptans, thiophenes or other organic sulfur compounds, a hydrodesulfurization stage may also be needed to convert them into H2S. The zinc oxide bed then captures the residual H2S before it can reach the downstream catalyst.
This division of duty matters. Sending an uncontrolled bulk sulfur load directly to a small ZnO guard bed can consume it quickly and bring the next changeout forward. For a wider view of suitable process streams, see applications of zinc oxide desulfurizers in industrial gas purification.
How Does a ZnO Bed Remove H2S?
The main gas-solid reaction is:
ZnO + H2S → ZnS + H2O

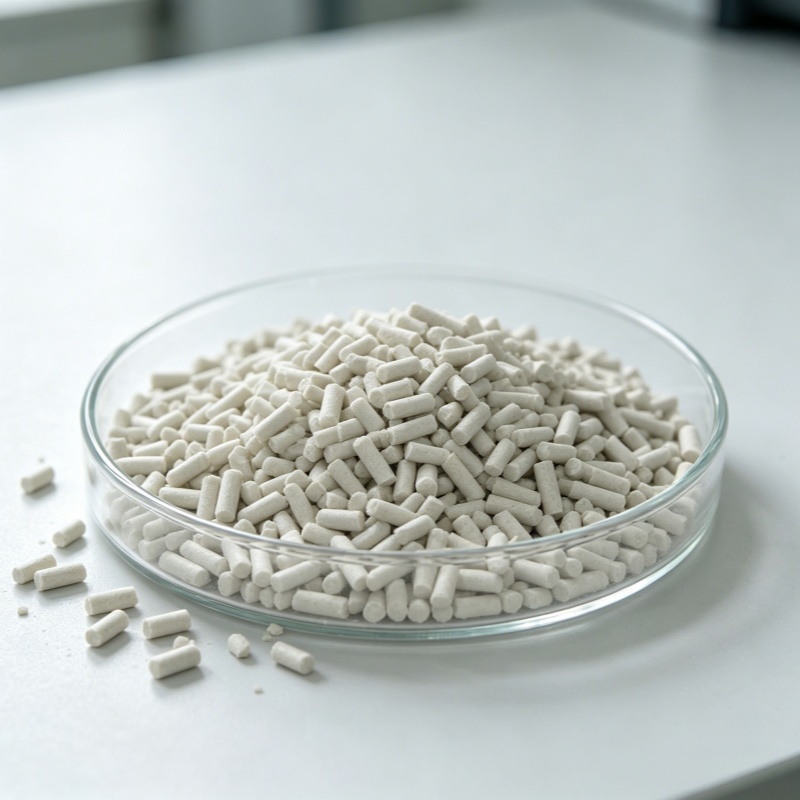
Zinc oxide is converted into zinc sulfide as the reaction front moves through the pellet. For that reason, the material is more accurately described as a reactive sulfur sorbent, although buyers commonly search for a zinc oxide desulfurization catalyst or H2S removal catalyst.
The reaction starts near the accessible pellet surface. H2S must then diffuse through the reacted layer to reach unused ZnO in the core. Pore structure, formulation and operating temperature therefore influence usable sulfur capacity. A high laboratory ZnO content does not automatically mean a long field cycle.
The purchasing number to compare is breakthrough sulfur capacity at a stated test temperature, not ZnO content by itself.
Select the Grade Around the Actual Gas Temperature
The vessel inlet temperature is the first selection gate. Using a conventional high-temperature ZnO product in a cool bed can leave capacity underused. A low-temperature formulation may be the better fit when additional feed heating is impractical.
| HONREL grade | Published operating range | Published breakthrough sulfur capacity | Best starting point for evaluation |
|---|---|---|---|
| HY310-C | 0–150°C | 30°C에서 ≥10 wt% | Low- and normal-temperature natural gas polishing |
| 티305 | 150~400°C | 20 중량% 이상 | Standard elevated-temperature ZnO guard-bed duty |
| HY306-G | 150~450°C | 220°C에서 20wt% 이상; 350°C에서 30wt% 이상 | High-temperature service where usable capacity and run length are priorities |
HONREL publishes an outlet H2S value below 0.1 ppm for these grades under the stated process conditions. That figure should not be separated from the feed composition, temperature, flow, pressure and vessel design. The final recommendation must be based on the complete duty, not one catalogue line.
You can review related gas-purification materials in HONREL’s industrial catalyst range.
Organic Sulfur Changes the Treatment Scheme
Standard ZnO is strongest on H2S. It should not be assumed to remove every sulfur species in natural gas at the same rate.
HONREL’s promoted zinc oxide grades are designed to convert or absorb simpler compounds such as COS and CS2 under suitable conditions. Mercaptans and stable thiophenic sulfur may require upstream hydrogenation before the ZnO bed. Temperature, hydrogen availability, residence time and the exact sulfur speciation decide whether direct capture is realistic.
If a gas analysis reports only “total sulfur”, ask for the split between:
- H2S
- COS and CS2
- Mercaptans
- Sulfides and disulfides
- Thiophenic sulfur
This avoids a common commissioning problem: an H2S bed performs as designed, but untreated organic sulfur still reaches the process outlet.
What Shortens the Zinc Oxide Desulfurization Catalyst Lifecycle?
A short cycle is often blamed on zinc oxide desulfurization catalyst decay. In practice, the bed may be consumed, bypassed or fouled rather than chemically “deactivated”.
| Plant signal | Likely cause | What to check before changing material |
|---|---|---|
| Outlet H2S rises earlier each cycle | Higher inlet sulfur load, increased flow or poor capacity utilisation | Inlet H2S trend, total gas flow, bed temperature and actual loaded mass |
| Fast breakthrough after startup | Channeling, uneven loading, a leaking support screen or an undersized bed | Loading record, bed level, distributor condition and vessel dimensions |
| Differential pressure keeps rising | Pellet breakage, fines, dust, oil mist or liquid carryover | Pressure-drop trend, filters, separators, condensate control and spent-bed condition |
| H2S slip follows a temperature change | Grade outside its useful reaction window | Minimum, normal and maximum inlet temperatures—not the design value alone |
| Total sulfur remains high while H2S is controlled | Organic sulfur is not being converted or captured | Sulfur speciation, upstream hydrogenation and hydrogen content |
| Unused ZnO remains in spent pellets | Diffusion limitation or premature breakthrough | Pellet structure, space velocity, operating temperature and flow distribution |
Apparent zinc oxide desulfurization catalyst loss can also come from oil, tar, dust or condensed hydrocarbons sealing the pore entrances. These contaminants should be removed upstream. Strong pressure or flow swings can disturb the bed, while poor loading can create voids and gas bypass.
Mechanical properties matter here. Pellet crush strength and abrasion resistance help limit fines, but careful screening, sock loading where appropriate and proper hold-down arrangements are still required.
Bed Life Starts With a Sulfur Mass Balance
Service life is not a fixed number of months. It depends on how much sulfur enters the vessel and how much usable capacity the loaded bed delivers before the agreed breakthrough limit.
For a first estimate, the buyer should provide:
- Normal, minimum and maximum gas flow.
- Inlet H2S and its expected variation.
- Required outlet H2S or total sulfur limit.
- Operating temperature and pressure range.
- Bed volume and current loading mass.
- Target run length between changeouts.
A lead-lag arrangement can give the plant more warning and allow the second vessel to protect the downstream unit when the lead bed approaches breakthrough. Regular outlet analysis is still essential. Calendar age alone is a poor replacement trigger.
If an existing charge is no longer meeting its run length, use HONREL’s zinc oxide desulfurizer replacement guide to compare the incumbent material with HY310-C, T305 or HY306-G.
What Should You Send With an RFQ?
“Natural gas H2S removal” is not enough information for reliable selection. A useful enquiry gives the supplier enough data to check chemistry, contact time, bed quantity and mechanical fit.
| RFQ data | Why HONREL needs it |
|---|---|
| Full gas composition | Identifies hydrogen, CO2, oxygen, water and other components that influence the bed |
| H2S at inlet and required outlet | Defines the sulfur duty and breakthrough target |
| COS, CS2, mercaptans and total sulfur | Shows whether upstream conversion may be required |
| Flow, pressure and temperature range | Supports GHSV and operating-window checks |
| Water or hydrocarbon dew point | Flags condensation and pore-blocking risk |
| Vessel diameter, bed height and volume | Supports loading quantity and superficial-velocity review |
| Current product TDS and pellet size | Makes replacement comparison faster |
| Loaded mass, cycle length and breakthrough history | Helps separate product capacity from process upset |
| Differential-pressure history | Indicates fines, fouling, compaction or maldistribution |
| Required quantity, destination and delivery date | Allows an export-ready supply proposal |
Do not order only by copying the previous tonnage. A change in bulk density or pellet geometry can change the loaded mass, bed voidage and pressure drop even when the vessel volume stays the same.
Source the Right Natural Gas ZnO Grade From HONREL
Buyers looking for an worldwide producer of zinc oxide catalyst for natural gas desulfurization need more than a generic certificate. The supplier should be able to match the formulation to the temperature window, compare breakthrough capacity on the same test basis and check the quantity against the existing vessel.
HONREL offers three defined ZnO grades rather than presenting one formulation as a universal answer. We can review a new unit or cross-check an incumbent desulfurizer using the current TDS, gas analysis and operating record. Read more about HONREL as a zinc oxide desulfurization manufacturer.
For a useful recommendation, HONREL에 문의하세요 with the RFQ data above. If the current bed is breaking through early, include the inlet and outlet sulfur trend, temperature profile, differential pressure and a photo of the spent material. That gives our team a better starting point than ZnO percentage alone—and helps you buy a grade that fits the plant instead of another catalogue match.